1. Why Impellers Are Difficult to Machine
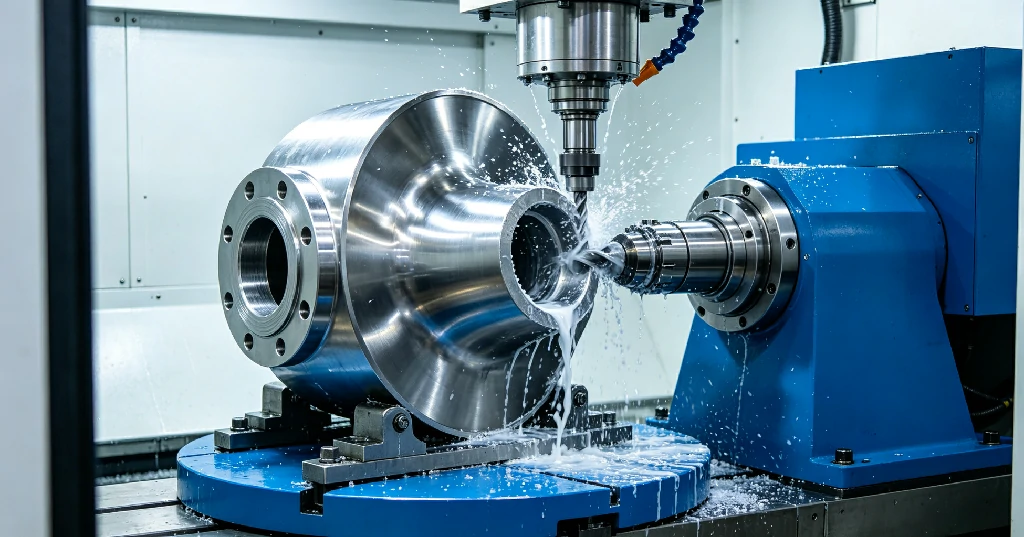
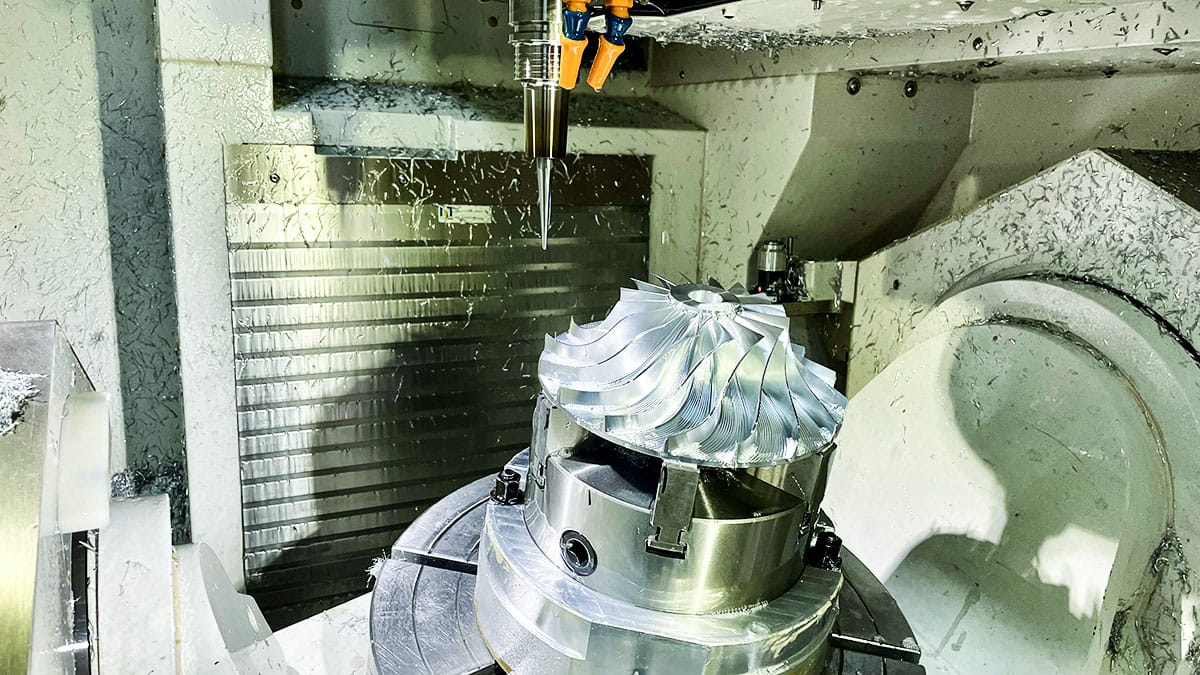
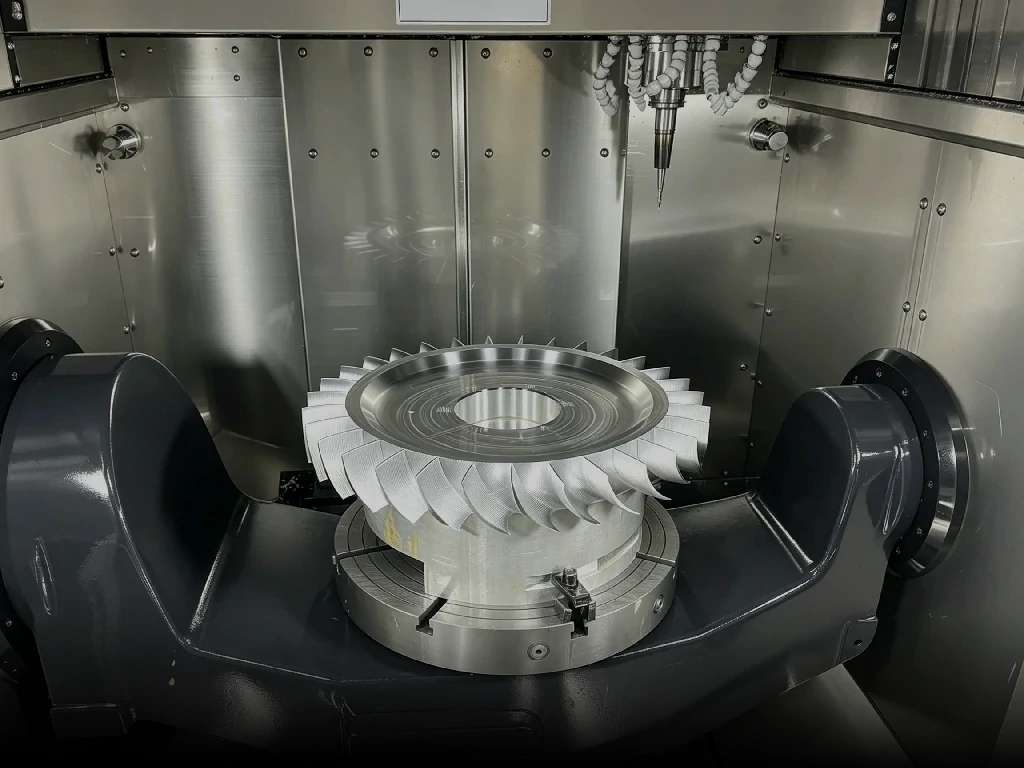
Impellers are critical components in aerospace engines, turbochargers, compressors, cryogenic pumps, and power-generation turbines. Their complex geometry—including twisted blades, deep flow channels, and thin walls—makes them one of the most demanding parts for CNC machining.
Conventional 3-axis machining requires multiple setups, increasing alignment errors and compromising surface quality. Simultaneous 5-axis machining eliminates these limitations by enabling:
- Single-setup machining with higher positional accuracy
- Continuous optimal tool orientation
- Surface finish of Ra 0.8–1.6 μm
- Up to 40% shorter machining cycles

2. Choosing the Right Machining Strategy
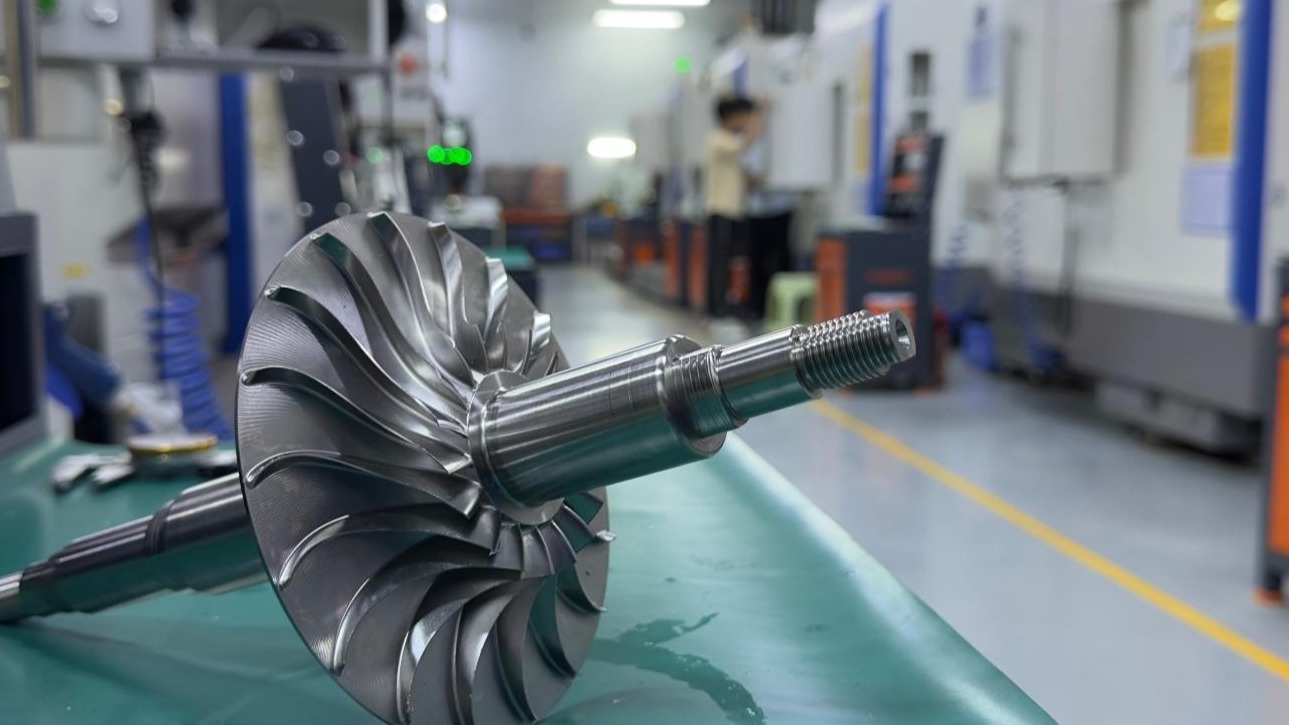
End Milling vs. Flank Milling
| Blade Geometry | Recommended Strategy | Productivity |
|---|---|---|
| Free-form twisted blades | End milling | Standard |
| Ruled surfaces | Flank milling | 40–60% faster |
Rule: If the ruled-surface fitting error is ≤0.02 mm, choose flank milling; otherwise use end milling.
Tool Selection
| Operation | Recommended Tool |
|---|---|
| Roughing | Corner-radius end mill |
| Semi-finishing | Corner-radius end mill |
| Free-form finishing | Ball-nose end mill |
| Ruled-surface finishing | Tapered barrel cutter |
Best Practice: Avoid ball-nose tools during roughing—they typically reduce material removal efficiency by around 30%.
Tool Rigidity: Keep tool overhang within 4× the cutter diameter (≤4D) whenever possible.
3. Recommended Cutting Parameters
Roughing
| Material | Cutting Speed (m/min) | Feed (mm/tooth) | DOC (mm) |
|---|---|---|---|
| Aluminum | 200–400 | 0.08–0.15 | 2–4 |
| Stainless Steel | 100–150 | 0.05–0.10 | 1–2.5 |
| Titanium | 50–80 | 0.03–0.06 | 1–2 |
| Inconel | 50–100 | 0.02–0.05 | 0.8–1.5 |
Use ≥70 bar coolant pressure when machining titanium or nickel-based alloys.
Finishing
For finishing, step-over has the greatest influence on surface quality.
| Step-over | Expected Surface Finish |
|---|---|
| ≤0.10 mm | Ra ≤0.8 μm |
| 0.10–0.20 mm | Ra 0.8–1.2 μm |
| 0.20–0.30 mm | Ra 1.2–1.6 μm |
| >0.30 mm | Generally unacceptable |
Recommendation: Maintain a finishing step-over between 0.08–0.20 mm for most impeller applications.
4. Titanium & Inconel Machining Best Practices
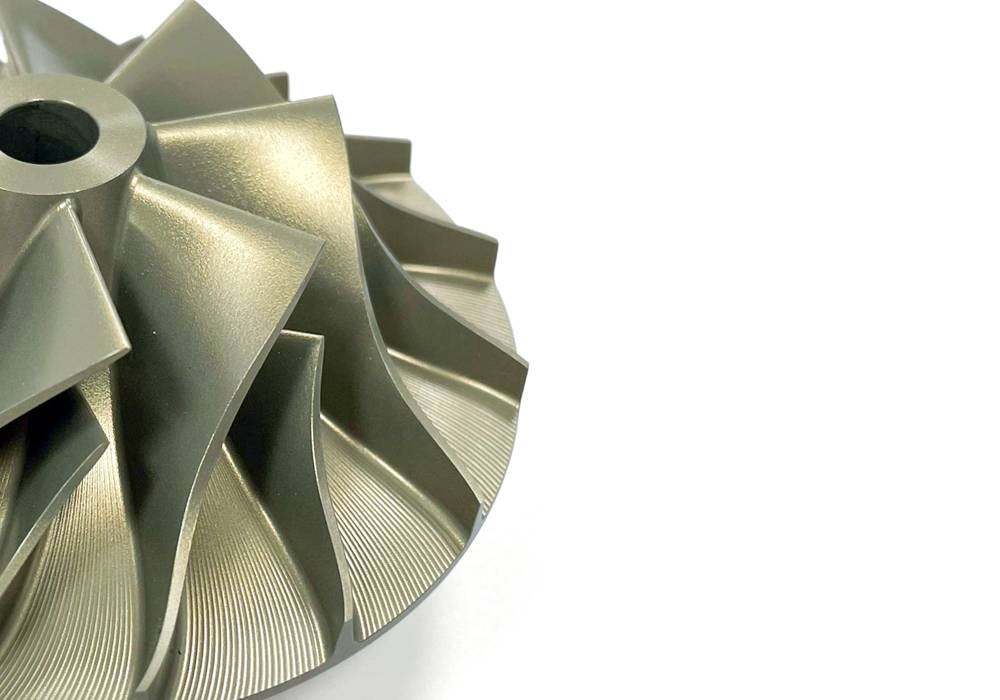
Heat-resistant alloys demand strict process control.
Follow these three rules:
- Use high-pressure coolant (≥70 bar) to control cutting temperature.
- Maintain continuous tool engagement to prevent work hardening.
- Monitor flank wear regularly and replace tools at approximately 0.15 mm wear.
Preferred coatings: AlTiN or TiAlN.
5. Controlling Thin-Wall Deformation
Thin impeller blades are highly susceptible to deflection.
Prioritize improvements in this order:
- Reduce tool overhang (≤4D) — the most effective solution.
- Apply high-pressure coolant to minimize thermal distortion.
- Use adaptive feed control to reduce cutting forces.
Tip: Excessive tool overhang is responsible for most blade deformation issues.
6. CAM Software Selection
Dedicated impeller machining modules dramatically reduce programming time and improve machining reliability.
| Function | Generic 5-Axis CAM | Dedicated Impeller Module |
|---|---|---|
| Programming | Manual intensive | Automated |
| Collision avoidance | Limited | Full machine simulation |
| Tool-axis optimization | Manual | Automatic |
| Flank milling | Basic | Optimized |
Recommended solutions
- hyperMILL Multi-Blade
- Siemens NX Blade
- OPEN MIND Impeller Module
Key CAM Settings
- Tool tilt angle: 5–15°
- Circular lead-in/out
- Programming tolerance ≤ 1/3 of part tolerance
- Safe retract height ≥ blade height +10 mm
7. Inspection Requirements
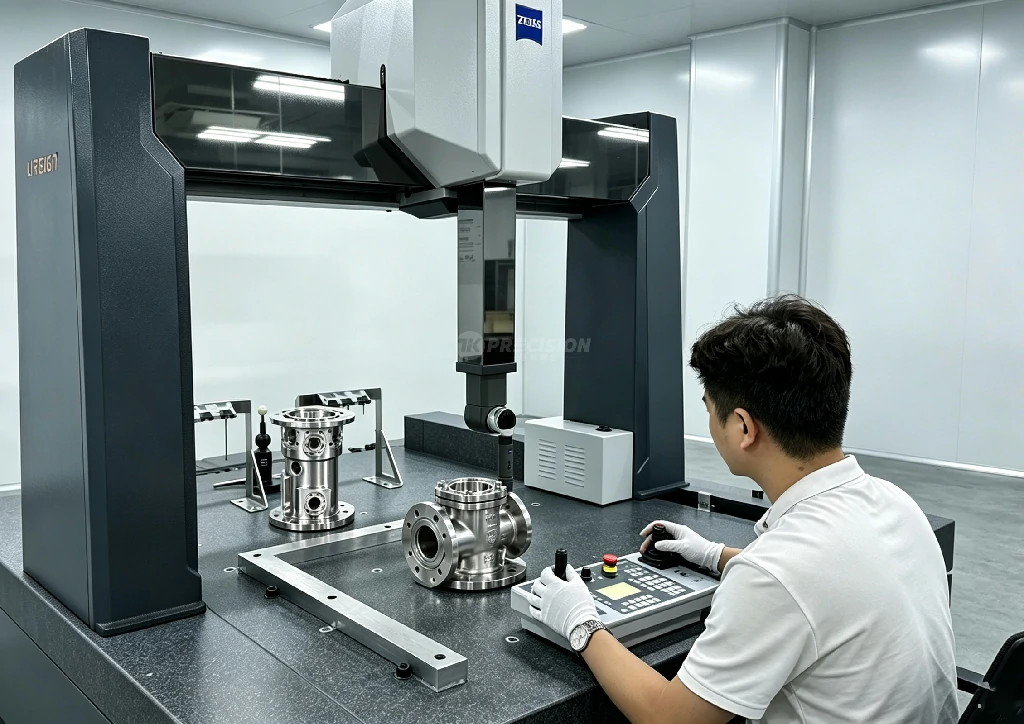
Every finished impeller should be verified for geometry, surface quality, and balance.
| Inspection | Acceptance Standard |
|---|---|
| Blade profile | ≤0.05 mm |
| Surface roughness | Ra 0.8–1.6 μm |
| Dynamic balance | ISO G2.5 or better |
Avoid these common mistakes
- Too few CMM measurement points
- Measuring profile without blade thickness
- Performing only low-speed balancing for high-speed rotors
8. Troubleshooting Guide
| Problem | Primary Cause | Recommended Action |
|---|---|---|
| Poor surface finish | Excessive step-over | Reduce to ≤0.15 mm |
| Chatter | Excessive tool overhang | Keep ≤4D |
| Dimensional error | Tool wear or inadequate coolant | Replace tool / increase coolant pressure |
| Short tool life | Excessive cutting speed | Reduce cutting speed by ~20% |
| Collision | Incomplete simulation | Run full machine simulation |
9. Key Takeaways
Remember these three principles:
- Choose flank milling whenever blade geometry allows—it offers the highest productivity.
- High-pressure coolant is essential when machining titanium and Inconel.
- Dedicated impeller CAM software reduces programming time, improves reliability, and quickly delivers a return on investment.
If you’re machining a specific impeller, share your material, blade geometry, and tolerance requirements—our engineers can recommend an optimized machining strategy and cutting parameters.